Two production machines. Both ways of using Logivyx.
One project runs Logivyx as a neutral HMI on top of an existing Mitsubishi PLC. The other replaces the PLC entirely with the embedded Soft PLC.
Multi-Station Hose Assembly Line — a neutral HMI on a Mitsubishi PLC.
Five assembly and test stations, eight Keyence barcode scanners, a Modbus TCP torque controller and a biometric attendance database — brought together on one Logivyx panel above an existing MELSEC iQ-F PLC. Live station status, shift-wise production, recipes per product and operator traceability.
What Logivyx connects
- SLMPMitsubishi MELSEC iQ-F PLC — the existing controller stays in place
- 8 ×Keyence barcode scanners — part codes scanned and verified at each station
- MODBUSTorque controller over Modbus TCP — live tightening torque and angle
- SQLBiometric attendance database — who is logged in at which station
What the operator sees
- Sequence step and assembly status for every station, from hose leak testing to end-of-line testing
- Pass / fail / total counts per shift (A, B, C) and total production
- Current and previous cycle time per station
- Live torque and angle trend, monthly production chart and alarm log
- Product recipes that load the operation sequence of every station
- Operator log-in per station for full traceability
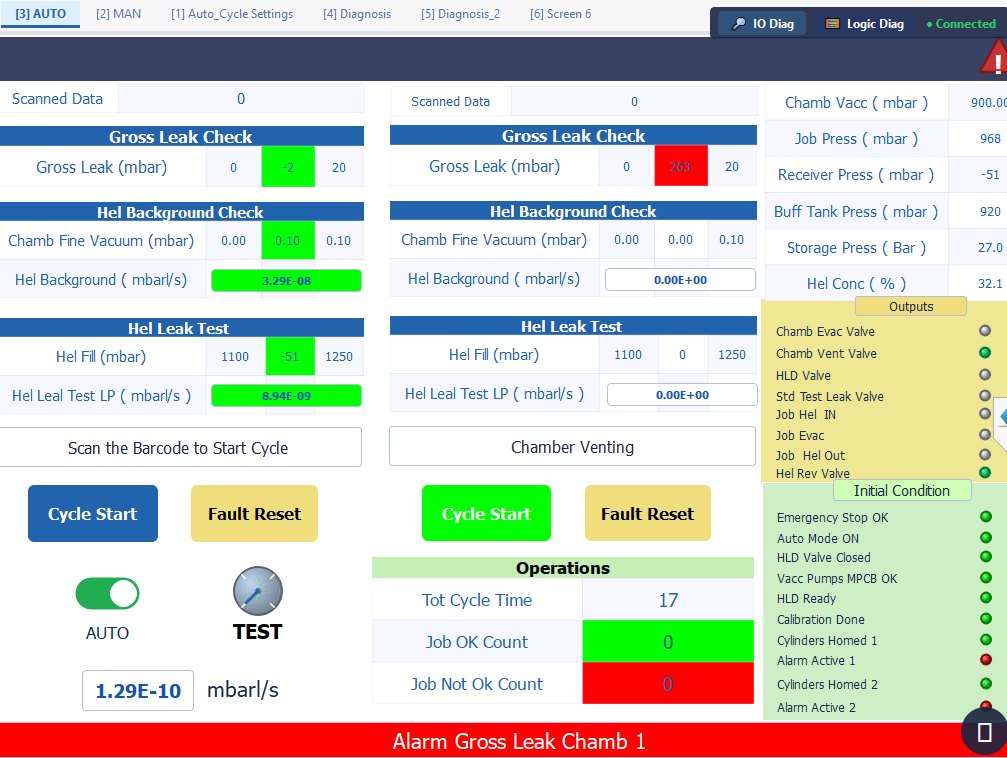
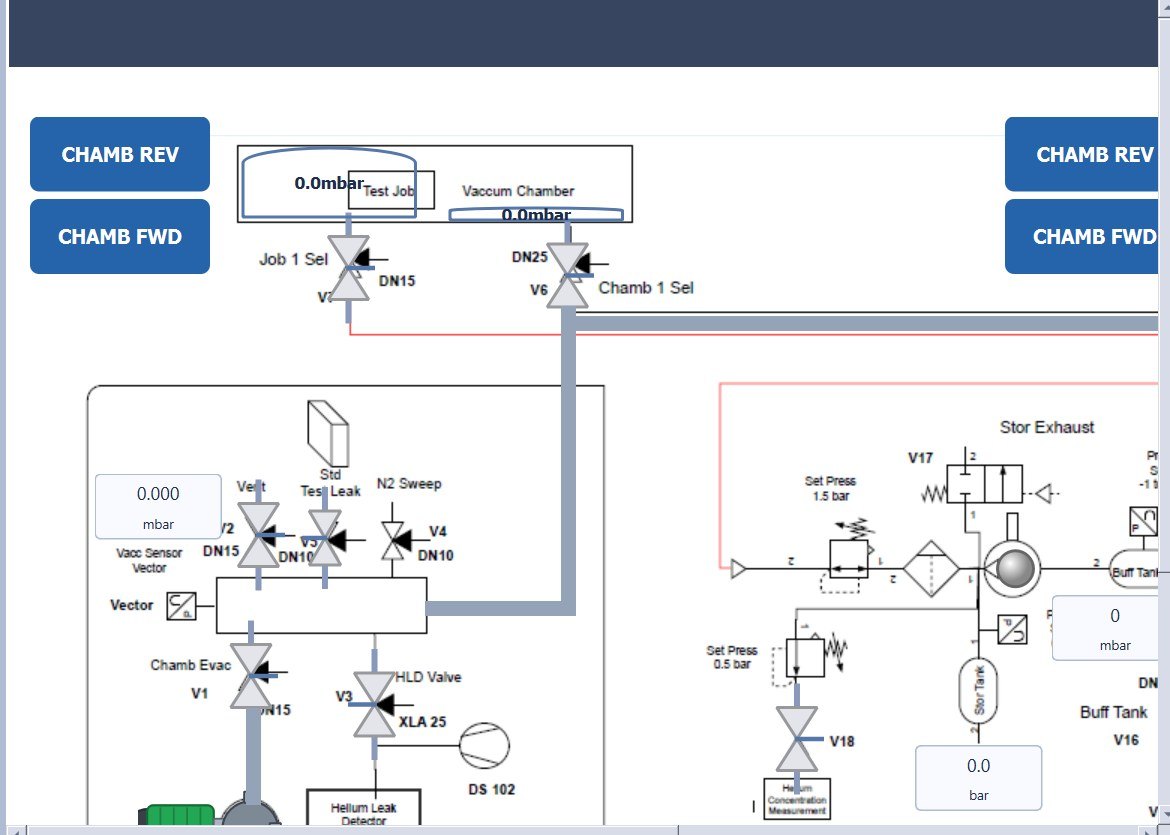
A helium leak testing machine with no separate PLC.
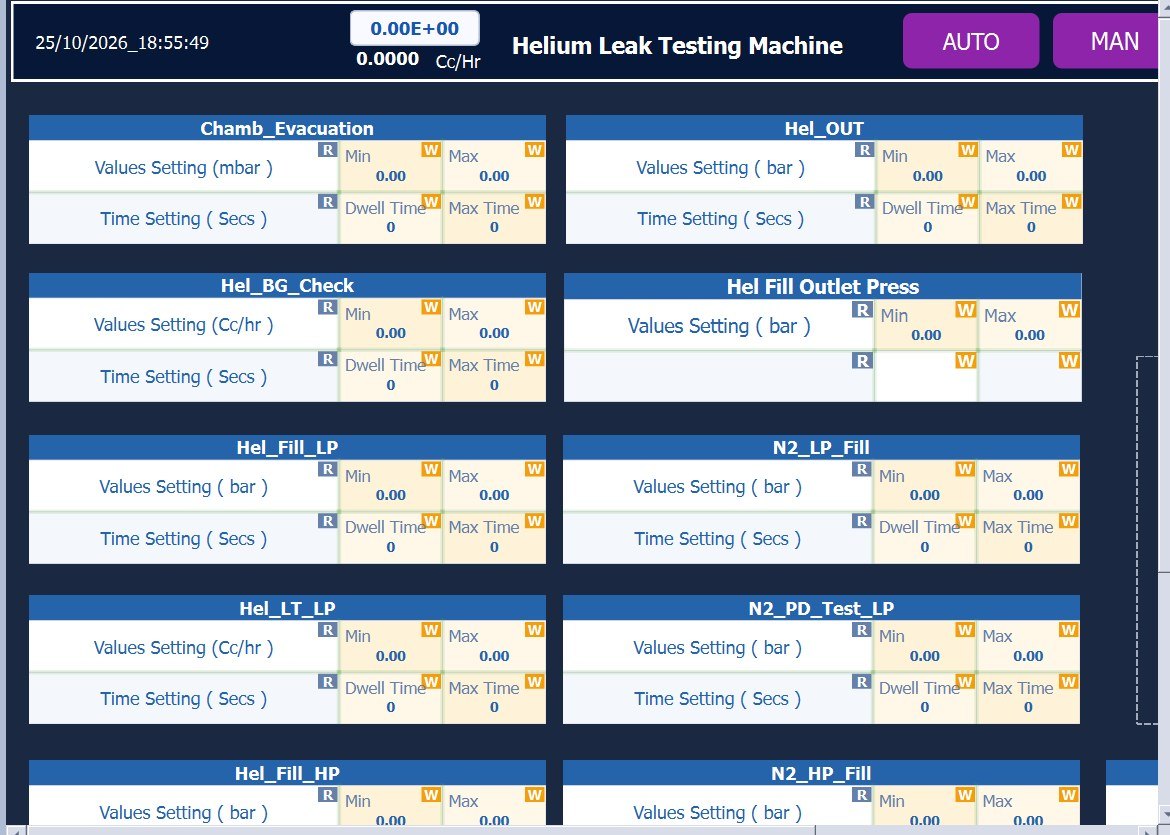
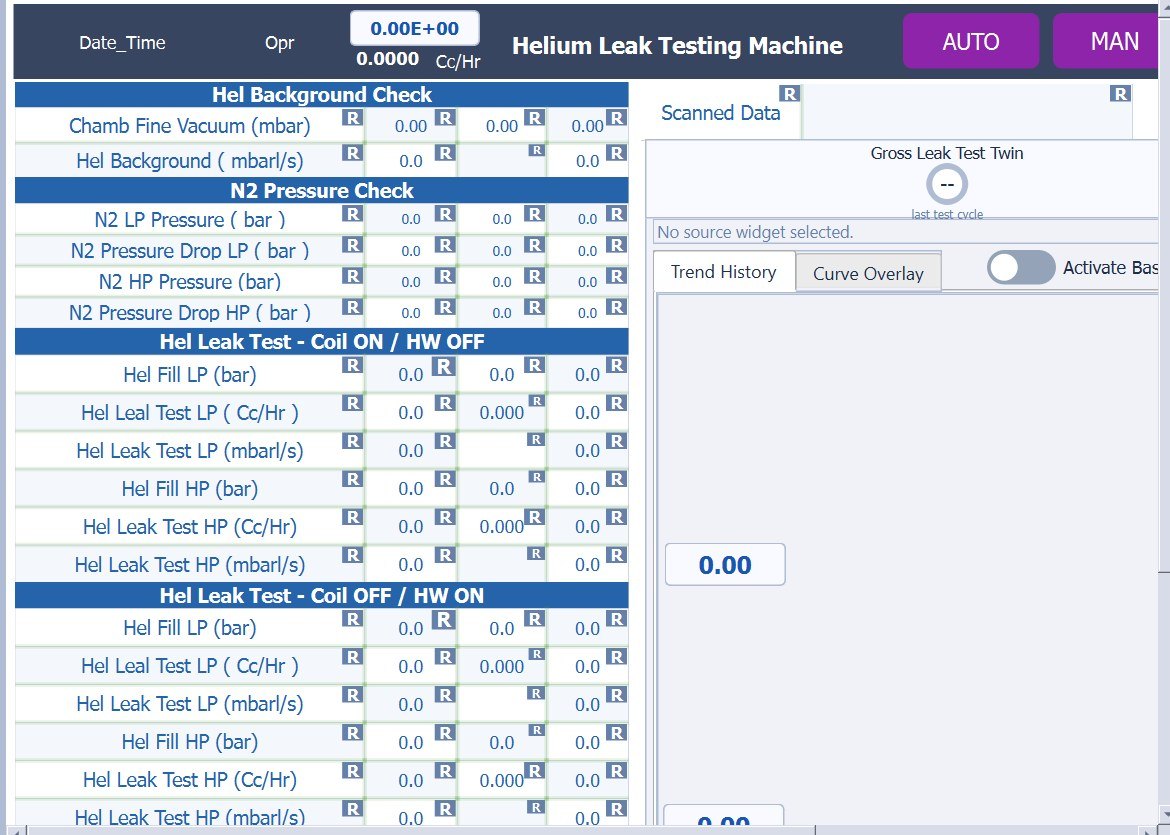
LSPL (Leckpreufung Systems) has built helium leak test machines since 2010. Their production machine is now engineered entirely in Logivyx — operator screens, P&ID process view, sequence-driven auto cycle, generated alarms and settings, and batch reports — running on a single industrial panel PC.
Two systems for every machine.
A conventional leak tester needs an HMI panel and a PLC CPU — two purchases, two engineering tools and licences, tags kept in sync by hand, and fault-finding split across two systems.
One project file, one panel PC.
The PLC CPU is gone from the bill of materials. Screens and logic share one tag database, and engineers trace a fault from the operator screen to the ladder rung without switching software.
[ADD: hardware cost saved per machine · commissioning time before/after · machines shipped]
“Logivyx has brought a tremendous improvement in our controls manufacturing lead time — along with a substantial cost reduction from eliminating the PLC hardware and expensive SCADA software licensing.”